Titanium Valves
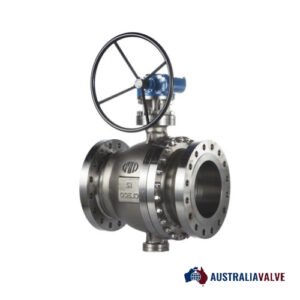
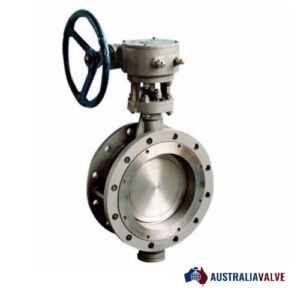
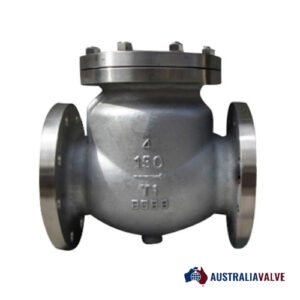
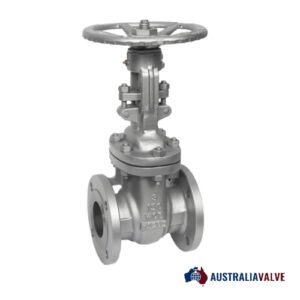
Titanium Valves deliver unmatched strength-to-weight ratios, exceptional thermal stability, and total immunity to severe chloride and acidic corrosion. Specifically engineered for Australia’s most challenging processing environments—including high-pressure acid leach (HPAL) nickel-cobalt mining, offshore oil and gas production, marine defense, and advanced chemical manufacturing—titanium valves eliminate catastrophic stress corrosion cracking (SCC) and severe pitting. At Australia Valves, our titanium category spans full-bore ball, gate, globe, check, butterfly, and control valves manufactured from high-grade commercially pure (CP) titanium and forged or cast titanium alloys. Key material grades include Unalloyed Titanium Grade 2 (ASTM B367 Gr. C-2 / ASTM B381 Gr. F-2) for maximum general corrosion resistance in oxidizing acids and moist chlorine gas, Titanium Grade 5 (Ti-6Al-4V / Gr. C-5) for high mechanical yield strength under pressure, and Titanium Grade 7 / Grade 12 (Gr. C-7 / Gr. C-12) alloyed with palladium or molybdenum-nickel for superior crevice corrosion protection in hot, concentrated brine and reducing environments. Designed and tested to stringent global standards including API 600, API 6D, ASME B16.34, ISO 9001, and NACE MR0175/ISO 15156, every titanium valve is supplied with full EN 10204 3.1 Material Test Reports (MTRs), Positive Material Identification (PMI), and pressure test certifications. Whether outfitting hydrometallurgical autoclaves or heavy-duty seawater desalination networks across Western Australia, Queensland, New South Wales, and Victoria, Australia Valves provides fully certified, project-ready titanium flow control solutions with fast nationwide delivery.
Showing all 4 results